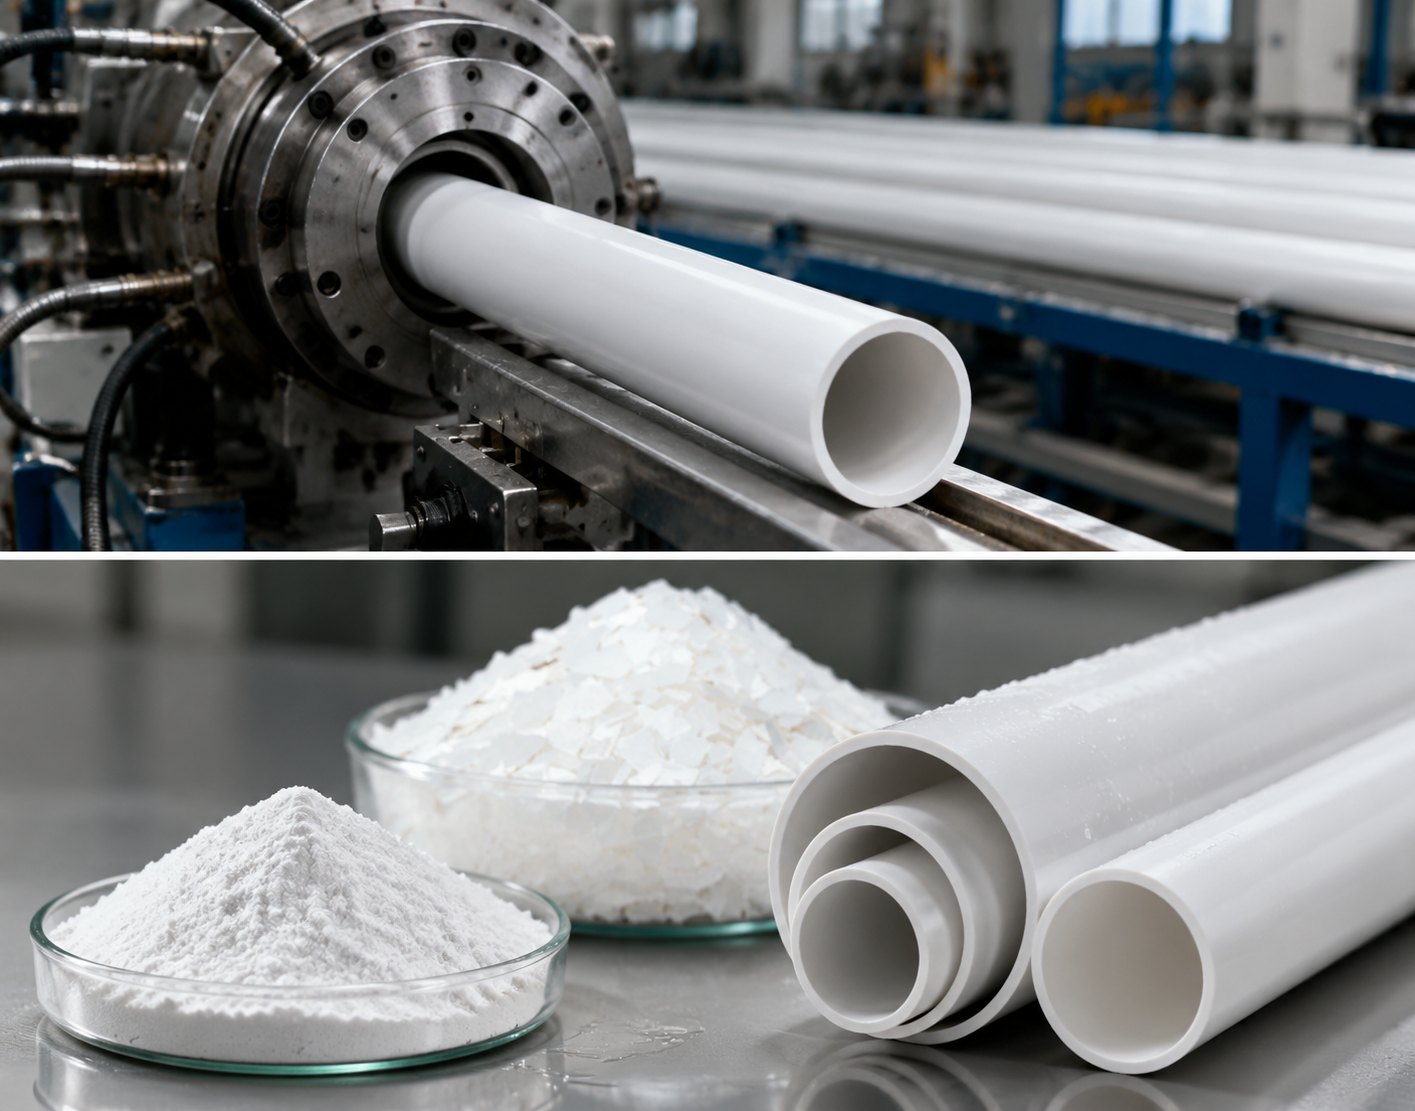
How to Select a PVC Foam Board Stabilizer for Cleaner Extrusion
Time : Sep 17, 2026 Vista : 675
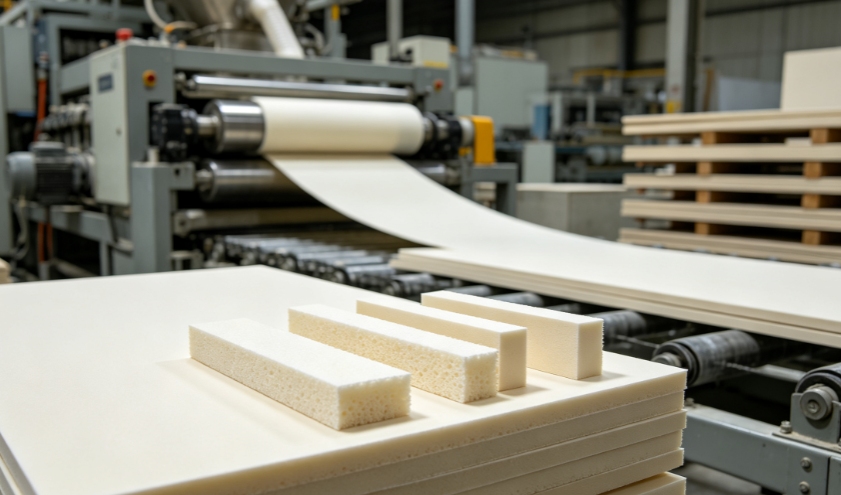
A PVC foam board can leave the die with acceptable color and still fail at the cut section. It may be too heavy, contain connected voids, or show density drift later in the run. These defects rarely point to one additive alone. They reflect how heat stability, plasticization, melt strength, lubrication, foaming, and line settings work together. As a PVC stabilizer supplier, we evaluate the full system before adjusting stabilizer dosage.
Why Foam Board Exposes Formula Imbalances Quickly
PVC is heat-sensitive. During high-temperature processing and mechanical shearing, it can release hydrogen chloride and enter an accelerating degradation cycle. The visible result may begin as yellowing and develop into discoloration or scorching. A stabilizer helps control this process by capturing hydrogen chloride and delaying further thermal degradation.
Foam board extrusion adds another challenge: the melt must retain a uniform cellular structure. Slow plasticization may leave particles, streaks, or a rough surface. Unbalanced lubrication may cause poor flow, plate-out, die buildup, or weak gelation. Insufficient melt strength can allow cells to connect or collapse.
This is why a PVC foam board stabilizer for extrusion should not be assessed by color alone. Initial color, long-term thermal stability, melt behavior, board density, cell section, surface finish, and die condition all belong to the same production review.
Read Board Defects as Processing Signals
Yellow edges do not automatically mean “add more stabilizer”
Yellow edges, yellow lines, black specks, and scorched material can indicate insufficient thermal stability. They can also result from excessive temperature, long residence time, high shear, dirty screens, or material decomposing in areas of buildup. Increasing stabilizer without checking these conditions can hide the signal without removing the cause.
We compare the defect with the temperature profile, screw speed, residence time, and the point when color begins to change. A stable startup board followed by darker mid-run sheets suggests a different condition from immediate yellowing at the die.
Pits, streaks, and rough surfaces often involve more than heat stability
Surface pits, drag marks, streaks, and poor gloss may come from inadequate plasticization, impurities, rough tooling, moisture, or unbalanced lubrication. Internal lubrication reduces friction within the melt. External lubrication forms a film between the melt and metal surfaces. Too little can contribute to sticking; too much can delay plasticization or increase migration and plate-out.
The stabilizer package, PVC lubricant, processing aid, filler, and temperature setting therefore have to be reviewed together. A smooth surface produced at only one narrow setting is not yet proof of a stable formula.
Low density is useful only when the cells remain sound
A light board is not automatically successful. Its cut section should show dense, uniform cells rather than large holes, continuous voids, or collapsed areas. Density should remain within the agreed range during normal production, not only in the best startup sample.
Foaming-agent balance, filler moisture, plasticization, melt strength, cooling, and line speed can all affect this result. The stabilizer contributes to the processing window, but it cannot compensate for every change elsewhere in the formula or extrusion line.
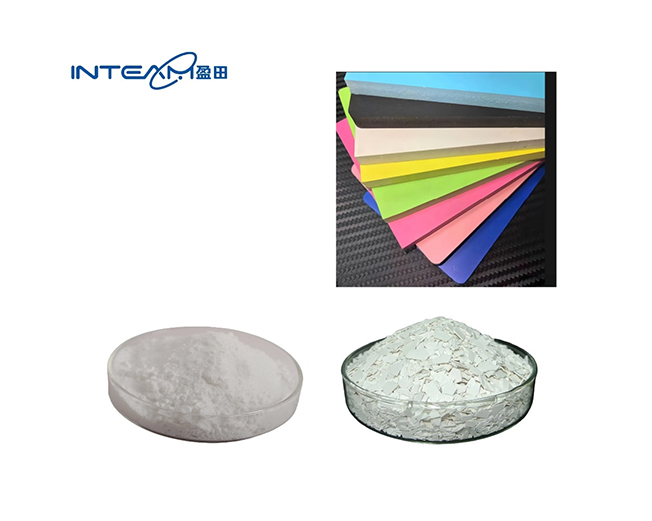
Where HB-88F Fits
Inteam HB-88F is positioned for foamed plates and micro-foamed plates. It is a estabilizador térmico compuesto containing tribasic lead sulfate, dibasic lead phosphite, lead stearate, antioxidant, lubricant, and heat-resistant additives. This one-package approach combines stabilization and processing functions in one system.
Under a suitable formula and line setup, HB-88F is designed to support uniform color, help avoid yellowing at thick walls and edges, and improve gelation and melt strength. These effects support flatter surfaces, better gloss, and fewer streaks or pits. Its lubrication contribution can reduce melt viscosity and torque and support smoother discharge without excessive external lubricant.
HB-88F is also intended to lower foaming temperature and support a light specific gravity with dense, uniform cells and fewer continuous voids. Its no-exudation processing behavior can help reduce material accumulation at the die head. The actual cleaning interval, however, must be confirmed on the customer’s equipment because filler level, lubricant balance, temperature, line speed, and raw-material consistency all influence die buildup.
A Useful Trial Tests the Formula, Not Just the Product
HB-88F is generally adjusted within 3-5 PHR. This is a starting guide, not a universal setting. The reference formulation allows 25-100 PHR of filler, and changes within that broad range affect plasticization, melt pressure, surface behavior, density, and lubrication demand.
When we review a trial, we keep the resin, filler, foaming agent, processing aid, lubricant balance, and temperature profile visible alongside the stabilizer dosage. Changing several variables at once makes it difficult to identify which adjustment improved the board.
Production observation | Variables to check | Useful acceptance evidence |
Yellow edges or color drift | Stabilizer dosage, local temperature, shear, residence time, buildup | Startup, mid-run, and late-run color samples |
High torque or unstable discharge | Plasticization, internal lubrication, temperature, filler loading | Torque record and steady discharge behavior |
Pits, streaks, or low gloss | Moisture, impurities, die condition, lubricant balance, gelation | Cooled surface samples and defect photos |
High density or poor cells | Foaming agent, melt strength, filler moisture, cooling, line speed | Density readings and cut-section samples |
Plate-out or die buildup | External lubrication, compatibility, temperature, run time | Time between cleaning and die-condition records |
Approval should compare more than one good sheet. Recording density, cut-section cells, gloss, edge color, torque, discharge, and die condition at several points shows whether the formula has a workable production window or only one successful moment.
The Stabilizer Route Must Match the Destination Market
HB-88F is a lead-containing composite stabilizer and is not suitable where lead-free or high-hygiene requirements apply. Approval should therefore begin with the finished-product application, customer specification, destination market, and applicable regulatory requirements. If the project requires a lead-free route, another stabilizer system should be evaluated instead of trying to qualify HB-88F for an unsuitable application.
Handling controls matter as well. HB-88F should be protected from moisture and stored in a cool, dry and well-ventilated storage area. It should be clearly identified and kept separate from lead-free or environmentally friendly product lines to reduce the risk of plant-handling errors. Operators should refer to the SDS (Safety Data Sheet) for the applicable safety and handling instructions.
What to Send Us Before a Foam Board Review
A useful technical discussion starts with actual production conditions. Provide the PVC resin grade, board type and thickness, filler type and loading, current stabilizer and dosage, foaming agent, processing aid, lubricant system, temperature profile, target density, equipment information, and destination market.
Defect samples add more value than a general description. Surface photos, cut-section images, density records, torque observations, boards from different stages of the run, and die-cleaning records help separate a thermal-stability problem from moisture, plasticization, lubrication, tooling, or cooling issues.
Our role as a PVC stabilizer supplier is not to treat dosage as an isolated answer. It is to help determine whether the stabilizer route fits the product, formula, process, and market requirements. For a foam board trial, contact Inteam with the current formulation and defect evidence so the discussion can begin with the real production constraint.
Preguntas frecuentes
What does a PVC foam board stabilizer do?
It helps protect PVC from thermal degradation during processing while contributing to the balance of plasticization, lubrication, melt behavior, surface quality, and foam-cell formation.
What dosage is recommended for HB-88F?
HB-88F is generally adjusted within 3-5 PHR. The final dosage should be verified against the resin, filler loading, additive package, extrusion equipment, and required board performance.
Why can PVC foam board develop yellow edges?
Possible causes include insufficient thermal stability, high local temperature, excessive shear, long residence time, uneven wall thickness, or decomposed material accumulating in the equipment.
How should cell structure be checked during a trial?
Measure board density and inspect cut sections from several stages of the production run. Acceptance should consider cell size and uniformity, continuous voids, collapse, and density drift together.
Is HB-88F lead-free?
No. HB-88F contains lead-salt components and should be considered only when the finished-product application, destination market, customer requirements, and handling controls allow a lead-containing stabilizer system.